Short answer: Quality control in unitised glazing is the factory inspection system that signs off every module before it ships: frame dimensions held to ±1.0–1.5 mm, diagonals within 1.5 mm, structural silicone batch-tested through a 7–21 day cure, and every glass, gasket, fastener and finish checked against its certificate. That evidence is what lets a 265–410 kg module hang on the slab in hours, without site rework.
Unitised glazing concentrates the quality risk of a whole facade into a factory process. A tower with 1,800 modules carries 1,800 opportunities for a dimension to drift, a seal to be missed or a gasket to be dropped into the wrong slot — and once the module is on the slab, correcting any of them costs ten to fifty times what it costs on the bench. This article sets out the tolerance chain, the structural silicone controls and the inspection gates that hold a unitised curtain wall to its specification, using the same performance targets we design to on our unitised glazing system: modules up to 1.5 × 4.0 m, system U-value ≈ 1.4 W/m²·K, SHGC ≤ 0.22, water tightness 750 Pa (ASTM E331) and structural wind up to 4.5 kPa (ASTM E330).
What Is Quality Control in Unitised Glazing?
Quality control (QC) in a unitised facade is a chain of documented checks — incoming material verification, in-process measurement, final inspection and batch traceability — that converts a specification into evidence. It differs from stick-built curtain wall QC in one decisive way: in unitised construction the module is the facade. There is no site phase in which a mis-glazed panel can be reglazed in place, so every check that a stick system would perform on the building is performed at the bench, on a jig, with calibrated tools and recorded against the module serial number.
Three documents carry that evidence: the mill certificate for every aluminium extrusion batch (EN 10204 3.1), the silicone and primer lot log tied to each module ID, and the dimensional report for each finished unit. On a tender for a Gulf or East African tower, ask bidders to submit all three as part of the quality plan — not just the test certificates for the mock-up performance tests.
Why Does Factory Assembly Produce Fewer Defects Than Site Glazing?
The factory wins on four controllable conditions that a site cannot guarantee:
- Environment. Structural silicone must cure between roughly 15–40 °C at controlled humidity. A factory hall holds that window all year; a floor of a tower in a 45 °C Gulf summer or a Nairobi rain week does not.
- Tooling. Modules are assembled on steel jigs that fix the squareness of the frame; site-assembled frames are squared by hand and spirit level.
- Repeatability. One glazing bench, one sealant application rate, one cure schedule — replicated across thousands of units — beats eighteen floors of changing crews, weather and access conditions.
- Inspection access. At the bench an inspector can see every gasket land and corner key. Twenty storeys up, behind a slab edge, he cannot.
This is why specification clauses for high-rise and coastal projects — where our system is rated to ISO 9223 corrosivity categories C4/C5 with an A2 fire classification — normally require factory glazing only, with site work limited to bracket set-out, lifting and module fixing.
What Tolerances Must a Unitised Module Hold?
The numbers that matter are the ones that keep two neighbouring modules compatible at the stack joint. A 1.5 × 4.0 m module weighing 265–410 kg (IGU from 6+12A+6 up to 8+16A+12) is built to these working tolerances on the jig:
| Check | Working tolerance | Why it matters |
|---|---|---|
| Module width / height | ± 1.0 mm | Keeps the sightline constant and the joint gap inside the gasket range |
| Diagonal difference (squareness) | ≤ 1.5 mm | A racked frame will not close the stack joint evenly along 4 m |
| Mullion straightness | ≤ 1.0 mm per 3 m | Bow shifts the glass bite and shows as a wavering reflection |
| Transom squareness | ≤ 0.5 mm per 300 mm | Protects IGU edge clearance and bite on all four sides |
| Glass-to-frame clearance | 3–5 mm per edge | Room for setting blocks and thermal movement without glass-to-metal contact |
| SSG structural bite | 10–15 mm (per design calc) | Carries the glass weight and wind suction to the frame |
| Fastener torque | Specified value ± 10% | Under-torque loosens; over-torque stresses the 6063-T5 extrusion |
Profile tolerances themselves are inherited from the extrusion die to EN 12020, and every batch of 6063-T5 arrives with its EN 10204 3.1 mill certificate; the anodised finish is verified at 5–20 µm film thickness (class AA15–AA25), 200–500 HV hardness and colour difference ΔE ≤ 2.5 by our anodizing partner in Guangdong, with neutral salt-spray resistance demonstrated from 500 to 4,000 hours depending on class.
How Is the Tolerance Chain Built From Slab to Module?
A module is never accurate in isolation — it is accurate relative to the slab. The chain absorbs deviation in stages, and each stage must be measured before the next is fixed:
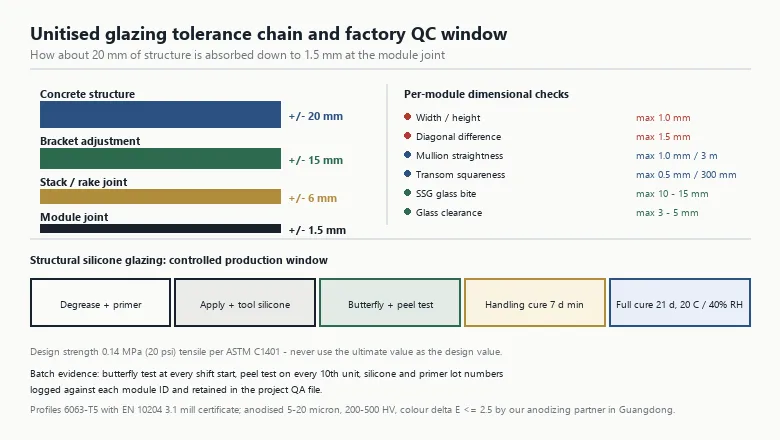
- Concrete structure: ± 20 mm. Surveyed with a total station; the theoretical grid is corrected to the as-built slab before any bracket is drilled.
- Bracket adjustment: ± 15 mm. Three-directional adjustable brackets take out the slab deviation (see the set-out tolerances in our installation sequence guide).
- Stack / rake joint: ± 6 mm. The joint design must stay functional across this travel — which is exactly why the two-stage seal and drainage path is dimensioned with reserve.
- Module joint: ± 1.5 mm. What remains after the factory holds the frame itself to ± 1.0–1.5 mm.
When a facade leaks or looks wrong, the root cause is almost always a stage that was skipped — brackets fixed to the theoretical grid instead of the surveyed one, or modules accepted without a dimensional report.
How Is Structural Silicone Glazing Controlled?
Where the glass is structurally bonded (SSG), the silicone line is the single most safety-critical joint in the module, and its QC is procedural rather than visual:
| Control point | Requirement |
|---|---|
| Sealant system | Two-part structural silicone tested to ASTM C1184 (or EN 15434 for EN 13098 systems) |
| Design strength | 0.14 MPa (20 psi) tensile design value per ASTM C1401 — never the ultimate strength |
| Surface preparation | Degrease, abrade where specified, primer applied and flash-off time observed |
| Mix verification | Butterfly test at every shift start; mix ratio logged from the metering machine |
| Adhesion verification | Peel test on production samples (typically every 10th unit) and on cured test pieces |
| Cure window | Minimum 7 days before handling at ≥ 20 °C and ≥ 40% RH; 21 days to full cure |
| Traceability | Silicone lot + primer lot + cure date recorded against each module ID |
A module must not leave the factory before its handling-cure period ends — which is why the production programme is coupled to the delivery programme, and why a supplier promising “glaze-and-ship-next-day” on SSG units is telling you something about their QC.
What Is Checked at Each Production Stage?
| Stage | What is verified | Evidence |
|---|---|---|
| Incoming materials | Alloy and temper (6063-T5), anodised film 5–20 µm / ΔE, IGU build-up 6+12A+6 to 8+16A+12 with Low-E, argon and warm-edge spacer, EPDM gasket hardness 60 ± 5 Shore A, fastener grade A2/A4 stainless | Mill certs, coating reports, IGU dew-point per EN 1279-2 / ASTM E2190 |
| Frame fabrication | Cut lengths, machining, corner key fit, thermal break assembly, fastener torque | First-article check per shift + jig repeatability |
| Glazing & sealing | Setting blocks, gasket engagement, SSG bite, silicone application and tooling | Butterfly + peel tests, per-module seal inspection |
| Cure & final | Dimensional report, diagonals, finish (no scratches, ΔE within batch), hardware function, label vs packing list | Signed module ID record; AQL sampling per ISO 2859-1 plus 100% visual |
| Packing | 40ft HC racks carrying 20–26 modules, corner protection, rack orientation matches the lifting sequence | Packing photos filed per shipment |
How Are Factory QC and Mock-Up Tests Linked?
The laboratory mock-up proves the design: air leakage Class A4 (EN 12152), watertightness RE 1200 (EN 12154) or 750 Pa under ASTM E331, structural performance to 4.5 kPa under ASTM E330, plus thermal and acoustic checks (system U ≈ 1.4 W/m²·K, SHGC ≤ 0.22, up to STC 42). Factory QC proves the production keeps that design. The bridge between the two is that the mock-up unit is built on the production jig by production staff, and the QC records of that exact module are appended to the test report. If a bidder tests a hand-built mock-up and then changes the gasket profile or silicone joint for production, the test evidence is void — require the mock-up QC file with every tender.
Which Defects Appear Most Often — and How Are They Prevented?
| Symptom on site | Typical root cause | QC prevention |
|---|---|---|
| Visible colour difference between modules | Anodising from unmanaged batches | ΔE ≤ 2.5 within batch; all modules of one elevation from one anodising batch |
| Water at the stack joint | Gasket not fully seated, drainage path blocked by sealant spill | 100% gasket engagement check; weep holes verified clear before packing |
| Glass rattling or edge contact | Missing/undersized setting blocks, clearance below 3 mm | Block size and position checked at glazing, clearance recorded per unit |
| Loose hardware after a year | Torque not controlled or thread-locker omitted | Calibrated torque tools + spot re-check at final inspection |
| Frame racked, joint gap uneven | Corner squares beyond 1.5 mm diagonal | Jig-locked assembly; diagonals on the dimensional report of every unit |
What Should the Quality Clause in Your Specification Require?
Copy these eight lines into the facade specification and most QC disputes disappear before they start:
- Factory glazing only for all vision and spandrel modules; no site reglazing of SSG units.
- Module dimensional report (width, height, diagonals) retained for 100% of units, available on request.
- Structural silicone per ASTM C1184 / EN 15434; butterfly test each shift, peel test each 10th unit, lot traceability per module ID.
- Anodised finish 5–20 µm (AA15–AA25), ΔE ≤ 2.5 within elevation; salt-spray class matched to ISO 9223 C4/C5 exposure.
- IGU dew-point compliance per EN 1279-2 / ASTM E2190, verified per production batch.
- EPDM gaskets 60 ± 5 Shore A with compression set ≤ 25% (ISO 815); no silicone-compatible incompatibility with the structural sealant.
- Fasteners A2/A4 stainless to ISO 9223 category, torque recorded on the module record.
- Mock-up unit built on the production jig by production staff; its QC file appended to the test report.
Key takeaways
- Unitised QC moves every check a stick system does on the building into the factory — the module must be right before it is lifted.
- The tolerance chain runs ± 20 mm (structure) → ± 15 mm (brackets) → ± 6 mm (joint travel) → ± 1.5 mm (module), and every stage must be surveyed, not assumed.
- SSG quality is procedural: certified sealant, butterfly and peel tests, a 7–21 day cure window and per-module lot traceability.
- The mock-up test proves the design; the module QC file proves production matches it. Ask for both.
- Finish consistency (ΔE ≤ 2.5 per elevation) and gasket engagement are the two defects most visible from the street — and both are 100% checkable at the bench.
Frequently asked questions
What does quality control cover in a unitised curtain wall?
Four gates: incoming materials (alloy certificates, anodised film thickness, IGU dew point, gasket hardness), frame fabrication on jigs, glazing and sealing with structural silicone batch tests, and a final dimensional report per module. Each check is recorded against the module serial number, so any unit on the building can be traced back to its material lots and inspection results years later.
What tolerances can a unitised module realistically hold?
Width and height within ± 1.0 mm, diagonal difference within 1.5 mm, mullion straightness within 1 mm over 3 m and glass clearance of 3–5 mm per edge. These are bench tolerances on a jig; the building itself is far less accurate, which is why brackets carry ± 15 mm of site adjustment and the stack joint is designed to travel ± 6 mm.
Why must structural silicone cure for 21 days?
Two-part structural silicone reaches handling strength in about a week but its full adhesion and cohesion develop over roughly 21 days at 20 °C and 40% relative humidity. Shipping a module early risks breaking the bond line while it is still green. The cure clock is logged per module ID, and the factory will not release a unit before its handling-cure period ends.
How is anodising quality checked between batches?
Film thickness is measured to confirm the 5–20 µm class range, hardness sits at 200–500 HV, and colour is compared within the batch to ΔE ≤ 2.5. All modules in one elevation are anodised in the same batch so the facade reads as a single surface. Salt-spray testing from 500 to 4,000 hours backs the durability claim for C4/C5 coastal exposure.
Does factory QC replace the facade mock-up test?
No — they answer different questions. The mock-up proves the design meets air, water, structural and thermal targets such as 750 Pa water tightness and 4.5 kPa wind load. Factory QC proves production repeats that design across every unit. The two connect when the mock-up is built on the production jig and its QC file is appended to the test report.
Need a unitised quality plan for your tower?
Send us the elevation, module count and exposure category. We return a project quality plan with the tolerance schedule, SSG cure programme, finish batch strategy and the inspection evidence set — aligned to SBC 901 / Mostadam documentation for Saudi projects. See the Unitised Glazing product page, the system specifications, the IGU selection guide and the anodised finish guide, or talk to our engineering team.